Order of Co-Extruded HDPE Pipes (White Exterior and Black Interior) for French Mining Project
Project Location: France / European Mining Infrastructure
Products Applied: DN450mm, SDR11 Co-Extruded PE100 Pipe (Double-Layer White/Black)
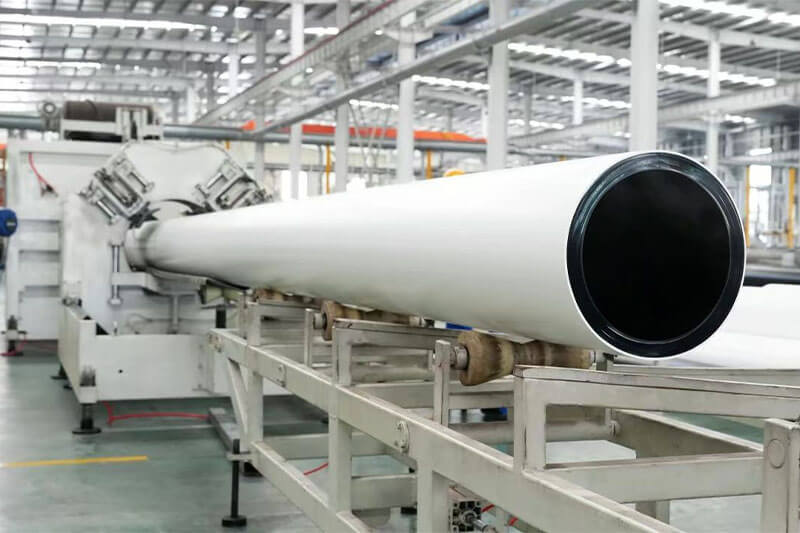
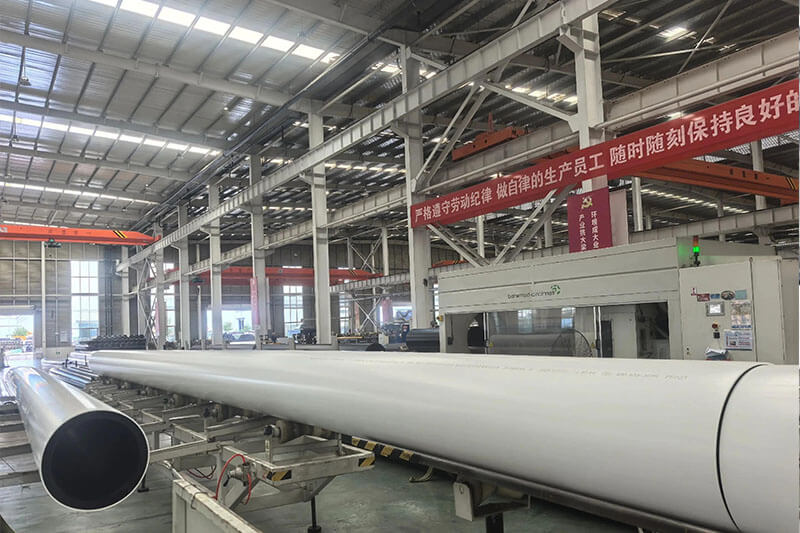
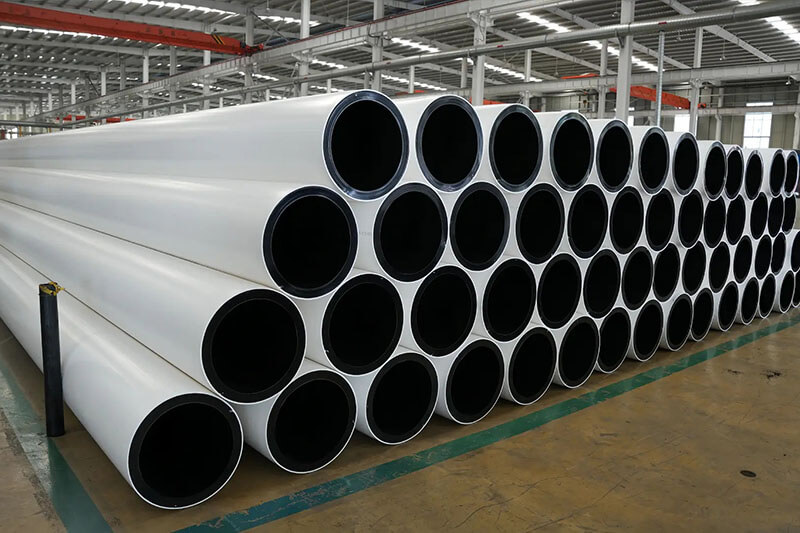
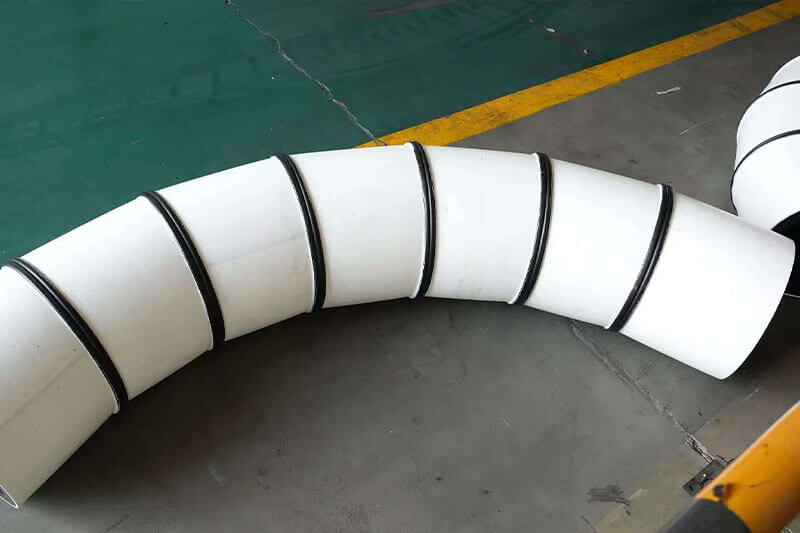
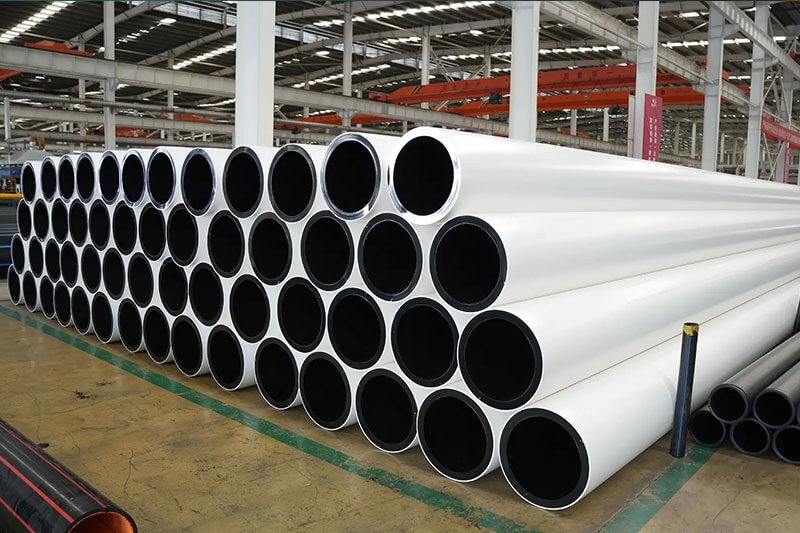
Custom-engineered DN450mm SDR11 double-layer co-extruded HDPE piping solution supplied by DEF PIPELINE for French clients, featuring high-reflectivity white outer layer for extreme UV resistance and black inner core for 100% light blocking.
Project Background & Customer Requirements
The French engineering and mining contractor approached DEF PIPELINE seeking a high-performance piping system capable of enduring severe environmental exposure. Traditional single-layer black polyethylene pipes deployed in open-pit mining environments often suffer from severe surface thermal expansion, UV degradation, and premature ageing under prolonged direct solar radiation.
To satisfy stringent European engineering and environmental mandates, the client placed strict parameters on the piping material:
- Thermal & UV Stability: Maximum solar reflectivity on the pipeline exterior to eliminate temperature-induced deformation.
- Biological Contamination Prevention: Total opacity in the interior to prevent algae growth and bacteria reproduction during fluid transport.
- High Mechanical Integrity: High ring stiffness and pressure-bearing performance (DN450mm, SDR11) resistant to rough handling on mining terrain.
- European Standard Compliance: Full conformance to EN 12201 and EN 13476 regulations with virgin material traceability.
DEF PIPELINE Engineered Solutions
Henan DEF Pipeline Technology Co., Ltd. developed a specialized customized solution deploying our proprietary dual-layer co-extrusion manufacturing line:
Advanced Co-Extrusion Technology
Manufactured on a state-of-the-art dual-layer synchronous co-extrusion line. The white exterior and black core achieve full molecular-level fusion during one-time thermal extrusion, completely eliminating any risk of delamination or structural separation under dynamic pressure cycles.
High-Reflectivity White Exterior
The outer layer is formulated with premium high-purity white masterbatch that provides exceptional sunlight reflectivity. By significantly lowering heat absorption, surface expansion and UV degradation in open-air environments are minimized. The high-contrast white finish also facilitates visual pipeline inspection and maintenance along the rugged project site.
100% Light-Blocking Black Core
The interior layer utilizes virgin PE100 with uniformly dispersed nano-carbon black particles. This ensures absolute 100% light-blocking capability, effectively preventing algae formation and microbial proliferation, keeping the interior clean, preventing bio-fouling, and securing fluid conveyance safety.
Certified Performance & Material Purity
Manufactured strictly with 100% imported prime virgin PE100 resin. The DN450 SDR11 specifications ensure heavy-duty impact strength and ring stiffness, fully compliant with EN 12201, EN 13476, and ISO global standards, safely providing 50+ years of engineered lifespan.
Client Feedback & Project Evaluation
“We are extremely satisfied with this collaboration. Henan DEF Pipeline fully understood our demanding specifications for open-air mining pipeline function. They delivered the co-extruded HDPE pipes with a black inner core and white exterior finish that exceeded our benchmarks in both mechanical quality and visual finish. In particular, the white exterior provides outstanding visibility across the active job site, vastly improving our safety management and on-site alignment. These pipes are instrumental to our project’s success, and we look forward to long-term future cooperation.”